| Cutting Technology |
Choose pure water cutting for soft materials such as rubber, foam, textiles, insulation, and some food products. Choose abrasive waterjet cutting for metals, stone, glass, ceramics, composites, and other hard materials. |
The cutting medium determines material compatibility, operating cost, consumable requirements, and waste generation. |
Confirm the full material list, thickness range, required edge quality, and whether abrasive media is permitted in the production area. |
| Operating Pressure |
Common industrial systems operate approximately between 2,760 and 6,200 bar (40,000–90,000 psi). Higher pressure can improve productivity but may increase energy consumption and component stress. |
Pressure affects cutting speed, maximum thickness, kerf quality, pump loading, and operating cost. |
Compare the rated pressure with the actual material thickness and production target. Do not exceed the lowest-rated component in the high-pressure circuit. |
| Water Flow |
Typical cutting-head flow is approximately 1.5–4.0 L/min per head, depending on orifice size, pressure, and machine design. |
Flow determines water consumption, pump capacity, drainage requirements, and cutting performance. |
Check the pump flow curve, number of cutting heads, water supply capacity, filtration capacity, and drain design. |
| Cutting Envelope |
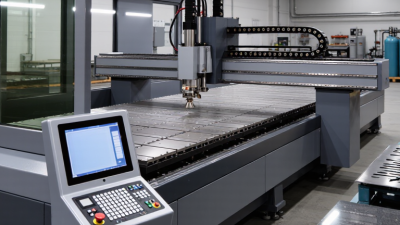
Select a working area that exceeds the largest regular sheet size by approximately 5–15%, while allowing space for clamping, loading, and operator access. |
An adequately sized table reduces repositioning, improves nesting efficiency, and lowers handling risk. |
Measure incoming material sizes, available floor space, access-door dimensions, lifting routes, and future production requirements. |
| Maximum Material Thickness |
Specify the maximum thickness for each material rather than relying only on a general machine rating. Cutting speed normally decreases as thickness and material hardness increase. |
Maximum thickness is affected by pressure, abrasive flow, nozzle condition, material properties, and required edge quality. |
Request cutting samples using the actual production material and define acceptable taper, roughness, dimensional tolerance, and piercing time. |
| Dimensional Accuracy |
For many industrial applications, practical accuracy is commonly in the approximate range of ±0.05–0.15 mm, depending on machine structure, calibration, material, thickness, and cutting strategy. |
Accuracy claims must reflect real operating conditions rather than ideal no-load positioning performance. |
Review test-part results, axis calibration procedures, thermal compensation, backlash control, and stated measurement conditions. |
| Abrasive System |
Use a controlled abrasive feed system with adjustable delivery. Common abrasive consumption may be approximately 0.2–1.0 kg/min per cutting head, depending on the orifice, pressure, material, and cutting speed. |
Abrasive flow affects cutting power, operating cost, edge quality, and disposal volume. |
Check abrasive hopper capacity, moisture protection, flow monitoring, blockage detection, dust control, and compatibility with the selected abrasive grade. |
| High-Pressure Safety |
The machine should include guarded high-pressure lines, pressure-rated fittings, automatic pressure relief, emergency stop functions, interlocked access doors, and protection against accidental startup. |
High-pressure water can cause injection injuries, component rupture, flying debris, and serious exposure hazards. |
Verify a documented risk assessment based on ISO 12100 principles or applicable local regulations. Inspect hoses, tubing, fittings, seals, and guards before use. |
| Control-System Safety |
Safety-related control functions should be designed and validated according to applicable requirements, such as ISO 13849-1 or equivalent regional standards. |
Reliable safety circuits help prevent unexpected motion, restart, door bypass, and loss of protective functions. |
Test emergency stops, interlocks, warning indicators, reset functions, and safe restart behavior during commissioning and periodic inspections. |
| Operator Protection |
Use a fully enclosed cutting area or an engineered splash and debris protection system. Operators should receive training in high-pressure hazards, abrasive handling, lockout/tagout, and emergency response. |
Water, abrasive particles, noise, and workpiece fragments may create physical and occupational hazards. |
Provide documented operating procedures, restricted access, suitable protective equipment, warning labels, and clear visibility of the cutting process. |
| Noise Control |
Waterjet cutting can generate high noise levels, particularly during piercing and cutting. Actual levels vary with enclosure design, pressure, material, and table configuration. |
Noise affects worker exposure, facility design, communication, and compliance with local occupational requirements. |
Measure sound pressure at operator positions. Consider a submerged cutting table, acoustic enclosure, hearing protection, and noise-reduction maintenance. |
| Water Quality |
Use filtered water with hardness, suspended solids, and chemical content controlled according to the pump and orifice manufacturer’s requirements. Reverse-osmosis or softened water may be required in areas with poor water quality. |
Water quality influences pump life, nozzle wear, seal performance, corrosion, and downtime. |
Test incoming water, install suitable filtration, monitor filter pressure drop, and prevent untreated water from entering sensitive high-pressure components. |
| Filtration and Sediment Management |
Provide staged filtration for incoming water and a practical method for collecting abrasive sediment and cutting debris from the tank. |
Efficient sediment removal protects pumps, reduces tank maintenance, and prevents blocked drains or contaminated discharge. |
Define filter replacement intervals, tank-cleaning frequency, sludge removal equipment, and safe handling procedures for collected waste. |
| Routine Maintenance |
Daily checks should include leaks, water level, nozzle condition, abrasive flow, emergency stops, interlocks, and abnormal noise. Periodic maintenance should cover seals, valves, filters, pump components, cables, and guide systems. |
Preventive maintenance reduces unplanned downtime and helps maintain consistent cutting quality. |
Use a maintenance log with inspection dates, operating hours, replaced parts, pressure readings, leak observations, and corrective actions. |
| Consumable Life |
Orifices, focusing tubes, mixing chambers, seals, filters, and pump wear parts require scheduled inspection. Service life varies greatly with water quality, abrasive type, pressure, and operating hours. |
Worn consumables can increase kerf taper, reduce accuracy, raise abrasive consumption, and create safety risks. |
Set replacement criteria based on measured cut quality, pressure stability, leakage, visual wear, and manufacturer-approved service limits. |
| Electrical Installation |
Provide a dedicated electrical supply sized for the pump, drive system, controls, lighting, and auxiliary equipment. The installation should include grounding, overcurrent protection, and an accessible disconnect. |
Correct electrical design supports safe operation, stable performance, and protection against overload or electrical faults. |
Confirm voltage, phase, frequency, rated current, short-circuit protection, grounding, cable routing, and local electrical-code compliance. |
| Floor and Foundation |
Install the machine on a level, rigid floor capable of supporting the operating weight, water load, workpieces, and dynamic forces. Follow the equipment supplier’s foundation and leveling tolerances. |
Insufficient stiffness or poor leveling can affect accuracy, vibration, drainage, and long-term machine reliability. |
Check floor loading, vibration sources, anchor requirements, leveling points, water-tank support, and access for maintenance. |
| Water Supply and Drainage |
Provide a stable water supply, backflow protection where required, overflow control, leak detection, and drainage designed for water mixed with abrasive sediment. |
Improper drainage can cause flooding, contamination, corrosion, and production interruptions. |
Confirm supply pressure and flow, drain capacity, floor slope, secondary containment, sediment management, and local wastewater rules. |
| Compressed Air and Utilities |
Some systems require clean, dry compressed air for abrasive control, valve actuation, mist reduction, or pneumatic components. Utility requirements depend on machine configuration. |
Moisture or inadequate air pressure can cause abrasive blockages, unstable cutting, and unreliable pneumatic operation. |
Check required pressure, flow, air quality class, dryer capacity, filtration, piping size, and condensate management. |
| Environmental Impact |
Evaluate electricity use, water consumption, abrasive consumption, sludge generation, noise, and the recyclability or disposal route of process waste. |
Environmental performance affects operating cost, permits, workplace conditions, and sustainability reporting. |
Calculate resource use per cutting hour or per finished part. Select efficient pumps, optimized cutting parameters, water reuse, and responsible waste handling where feasible. |
| Wastewater and Abrasive Disposal |
Collect and classify wastewater, used abrasive, metal fines, coatings, paint residues, and other contaminants before disposal or recycling. |
Cutting waste may contain regulated substances depending on the material being processed. |
Review local wastewater and solid-waste regulations. Keep waste streams separated when this improves recycling or simplifies compliant disposal. |
| Software and Data Connectivity |
Choose software that supports nesting, lead-ins, piercing control, kerf compensation, toolpath simulation, job records, and secure data backup. |
Good software reduces material waste, improves repeatability, and helps operators identify process problems. |
Check file compatibility, user access controls, backup procedures, simulation functions, remote-support policies, and offline operation capability. |
| Service and Spare Parts |
Maintain access to critical wear parts, filters, seals, nozzles, mixing tubes, pump components, and approved maintenance procedures. |
Spare-part availability directly influences downtime and production continuity. |
Define minimum stock levels, expected delivery times, technical support coverage, training options, and service documentation before purchase. |
| Total Cost of Ownership |
Compare purchase price with electricity, water, abrasive, consumables, labor, maintenance, waste treatment, downtime, and facility modification costs. |
The lowest initial price may not provide the lowest cost per finished part. |
Calculate cost per operating hour and cost per representative part using actual production volume, material thickness, abrasive rate, and maintenance assumptions. |
| Final Acceptance Test |
Require documented tests using representative materials, thicknesses, cutting speeds, abrasive settings, and dimensional tolerances. |
A practical acceptance test confirms that the machine meets production requirements before full deployment. |
Record cutting time, edge quality, dimensional accuracy, taper, consumable condition, noise, water use, abrasive use, and safety-function results. |