Top 10 Benefits of Waterjet Cutting Rubber?

Rubber looks simple on a drawing. On the shop floor, it can stretch, compress, and shift under a blade. Waterjet cutting rubber offers a different approach: a focused stream cuts without a conventional heated edge, helping preserve delicate profiles and reduce tooling contact. Yet results still depend on rubber formulation, thickness, pressure, nozzle condition, and fixturing. No process removes the need for testing.

Market context is useful, but it should not be mistaken for proof of rubber-specific performance. Grand View Research’s waterjet cutting machine market coverage tracks industry demand and technology trends; it does not establish a universal cost or productivity advantage for every rubber part. For technical grounding, Mohamed Hashish’s published work on waterjet technology discusses the process’s cold-cutting characteristics. In paraphrase, his research highlights the value of avoiding heat-related damage. That is relevant when a seal’s edge quality matters.

The benefits ahead are practical, not automatic. They include intricate shapes, narrow kerfs, and reduced heat exposure, alongside constraints such as water management and part movement. A small test cut can reveal more than a polished brochure. This guide examines ten potential benefits of waterjet cutting rubber, while keeping the trade-offs visible. Some figures vary by material and machine. That uncertainty deserves attention.
Top 10 Benefits of Waterjet Cutting Rubber?

What Is Waterjet Cutting, and How Does It Cut Rubber?

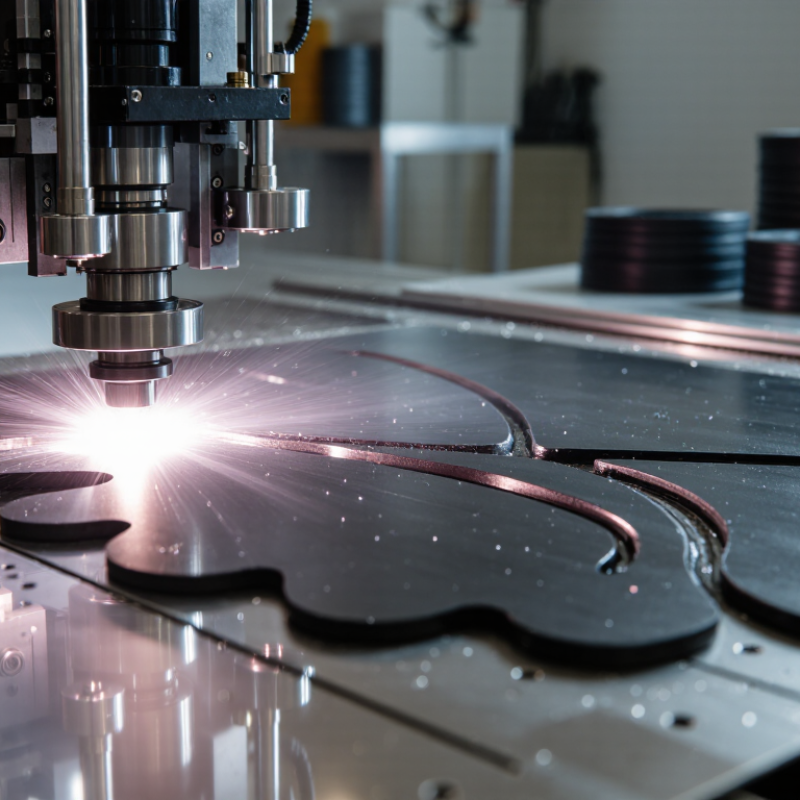
Waterjet cutting uses a narrow stream of pressurized water to slice through sheet material. For rubber, the process usually relies on water alone rather than added abrasive particles. The focused jet exits a small nozzle at high speed and follows a programmed path across the sheet. It cuts by eroding material along that path. No blade needs to press against the rubber.

A CNC system guides the cutting head, making it possible to produce gaskets, seals, and detailed profiles from digital drawings. The rubber is typically laid flat on a support bed, and the operator sets the pressure, feed rate, and nozzle distance for the material’s thickness and hardness. Small details matter. If the sheet shifts or stretches, even a precise path can produce an imperfect part.

Because waterjet cutting does not use a heated blade, it avoids a heat-affected edge that could otherwise harden or scorch some rubbers. It can also cut complex shapes without making a custom die. The finished edge is often clean, though very soft or elastic rubber may deform slightly under the jet. That part can be frustrating. A test cut helps confirm whether the chosen settings suit the specific compound before a full sheet is processed.

How Does Waterjet Cutting Compare with Other Rubber-Cutting Methods?

Top 10 Benefits of Waterjet Cutting Rubber

How Does Waterjet Cutting Compare with Other Rubber-Cutting Methods?

Waterjet cutting separates rubber with a high-pressure stream of water, sometimes mixed with abrasive material. Unlike a blade, it applies little mechanical force, which can help prevent soft sheets from stretching or shifting. It also avoids the heat produced by laser cutting, so edges are less likely to melt, harden, or discolor. For gaskets and intricate profiles, the narrow stream can produce clean details with minimal tooling. No heat. No blade wear.

Compared with die cutting, waterjet cutting can be more flexible for prototypes or short production runs because each design change may not require a new custom die. However, die cutting can be faster and more economical for large batches of simple shapes. Laser cutting offers speed and fine detail on some materials, but heat-sensitive rubber may produce fumes or altered edges. Results depend on the rubber compound, thickness, and machine settings. Waterjet cutting is not perfect: very soft rubber can deform under pressure, and the process may leave a damp edge that needs drying.

Tips: Ask for a sample cut using the exact rubber grade and thickness. Check edge quality, dimensional tolerance, and drying time before approving a full run. Small details matter. A test piece can reveal problems that a neat drawing will not.

What Are the Top 10 Benefits of Waterjet Cutting Rubber?

What Are the Top 10 Benefits of Waterjet Cutting Rubber?

Waterjet cutting offers a practical way to shape rubber without a hot cutting edge. Its first benefits are minimal heat damage and reduced risk of melting, scorching, or hardened edges. It can also limit mechanical stress, which helps flexible sheets keep their shape. A narrow cutting stream supports detailed profiles and smaller internal features. It handles varied thicknesses and rubber formulations, though settings must be tested for each material. There is no tooling die to manufacture or store, so short production runs and design changes can be more economical. Cuts can often be made directly from digital designs, reducing setup time and manual trimming.

The remaining benefits are clean edges, less secondary finishing, nesting flexibility, and repeatable shapes when pressure, speed, and nozzle distance are controlled. ASTM D412-16(2021), a standard test method for rubber tensile properties, underscores why preserving a sample’s condition matters: heat or distortion can affect how material behaves during testing. Waterjet cutting avoids a heat-affected zone, but it is not perfect. Soft rubber may flex, and abrasive particles can leave residue or rough edges. A trial cut is wise. Record the settings, inspect the edge, and check dimensions before scaling production. That small step can prevent a full batch of unusable parts.

Which Types of Rubber and Applications Suit Waterjet Cutting?

Waterjet cutting suits many sheet and slab rubbers, especially when parts need clean profiles without a heated blade. Natural rubber, EPDM, neoprene, nitrile, and silicone can often be cut this way. The best choice depends on thickness, hardness, and whether the material is reinforced. Check the supplier’s data and test a sample before production. Small details matter.

The process is useful for gaskets, seals, vibration pads, and custom liners. A shop can cut bolt holes and intricate outlines in one setup, which helps when parts must fit around pipes or machinery. It also avoids heat-affected edges, a benefit for heat-sensitive compounds. However, soft rubber may compress under the cutting stream, and thick or highly elastic sheets can produce tapered edges. Support the sheet evenly and tune pressure and feed speed for the material. Results vary.

Waterjet cutting can also handle rubber bonded to fabric or foam, but mixed layers may separate or cut unevenly. For dense rubber flooring, a test piece reveals whether the edge stays square and clean. Inspect the finished part, especially narrow tabs and small holes. A rushed setup can leave rough edges, even with a precise machine.

Top 10 Benefits of Waterjet Cutting Rubber — Which Types of Rubber and Applications Suit Waterjet Cutting?

Benefit How It Helps Rubber Types That Commonly Suit the Process Typical Applications Practical Considerations
1. No heat-affected zone Pure-waterjet cutting removes material mechanically, avoiding the thermal damage and heat discoloration associated with heat-based cutting methods. Natural rubber, EPDM, neoprene, nitrile (NBR), and silicone rubber Gaskets, seals, vibration pads, and components made from heat-sensitive elastomers Waterjet cutting is a cold process, but the workpiece should still be checked for water compatibility and post-cut cleanliness.
2. Suitable for many elastomer grades A range of flexible and firm rubber sheets can be cut with a waterjet when the pressure, speed, nozzle, and support setup are matched to the material. Natural rubber, EPDM, neoprene, NBR, silicone, and some polyurethane elastomers Industrial seals, protective covers, sheet components, and custom profiles Cutting performance varies with hardness, reinforcement, formulation, and sheet thickness; test cuts are useful for unfamiliar materials.
3. Handles intricate profiles A narrow jet can follow detailed outlines and internal features without requiring a dedicated cutting die for each design. Most homogeneous rubber sheet materials, including silicone and neoprene Custom gaskets, shaped seals, instrument pads, and prototype parts Very small holes and narrow slots depend on material thickness, jet diameter, and the required dimensional tolerance.
4. Low cutting force on the workpiece The process applies less direct mechanical force than many conventional blade operations, helping reduce compression during cutting. Soft natural rubber, silicone, EPDM, and flexible foam rubber Soft gaskets, cushioning pads, and delicate sheet components Soft materials can still shift, stretch, or deform; suitable fixturing and a stable support surface are important.
5. No hard cutting tool contacting the profile The cutting action does not rely on a blade rubbing along the finished edge, which can help avoid blade drag on flexible materials. Soft or tacky rubber sheets, including natural rubber and silicone Flexible seals, liners, and irregularly shaped rubber parts Part hold-down and careful lead-in and lead-out planning help prevent movement or edge defects.
6. Efficient for varied or changing designs Profile changes can generally be made by updating the cutting program rather than manufacturing a new profile-specific die. Rubber sheet grades used for prototypes, short runs, and custom production Product development, replacement parts, and low-volume gasket production Machine programming and setup are still required, and very high-volume work may favor dedicated tooling depending on part design.
7. Supports accurate repeat cutting Computer-controlled paths can reproduce programmed shapes consistently when the material is held flat and process settings remain stable. Neoprene, EPDM, NBR, and other dimensionally stable sheet rubber Repeat batches of seals, washers, and equipment gaskets Rubber may stretch or compress, so tolerances should account for material behavior as well as machine capability.
8. Can cut thick sheet material Waterjet systems can cut a range of sheet thicknesses, with suitable settings and equipment, without relying on a blade that must pass through the full sheet. Firm rubber sheet such as NBR, neoprene, and EPDM; some thicker elastomer stock Thick gaskets, industrial pads, and heavy-duty liners Maximum practical thickness depends on the machine, material, edge-quality requirements, and cutting speed; confirm with a sample cut.
9. Helps reduce profile-specific tooling Digital cutting paths can reduce the need for dedicated dies when producing custom shapes or multiple part designs. Rubber sheets in mixed sizes and varied profile designs Custom gasket sets, maintenance parts, and short-run components Material use and production cost depend on nesting, setup time, cut speed, and order quantity.
10. Broad application flexibility The same process can produce flat profiles in different shapes and sizes, making it useful across multiple industries and part types. Natural rubber, EPDM, neoprene, NBR, silicone, and selected polyurethane elastomers Automotive and machinery seals, electrical enclosures, HVAC gaskets, food-equipment seals, and cushioning parts Confirm that the selected rubber grade meets the application's temperature, chemical, weathering, and regulatory requirements.

Process note: Rubber sheet is commonly cut using a pure-waterjet rather than an abrasive jet. Waterjet suitability and achievable edge quality depend on the rubber formulation, hardness, thickness, reinforcement, machine setup, and required tolerance. Materials that absorb water or contain sensitive layers may need testing and appropriate drying or handling.

What Factors Should Be Considered When Waterjet Cutting Rubber?

Waterjet cutting can shape rubber without a heated blade, which helps avoid melted edges and heat-related changes. The result depends on the material, though. Natural rubber, silicone, and dense rubber sheet behave differently under the same setup. Check the grade, thickness, hardness, and reinforcement before choosing a cutting plan. A thin gasket may cut cleanly, while a thick, soft sheet can flex or compress.

No heat, but setup matters. The water pressure, nozzle condition, and cutting speed affect edge quality and accuracy. If the stream moves too quickly, small holes and tight corners may come out rough. Slower cutting can improve detail, but it may increase production time. Test a sample with the actual rubber whenever possible. Measure the finished piece after cutting, not just the digital drawing; rubber can relax or shift once released.

Support is another practical factor. The sheet should lie flat and remain secure without being stretched, since tension can distort the final shape. For narrow parts, consider how easily they may move or tear during cutting. Keep the work area and drainage system suitable for abrasive waterjet operations, if abrasives are used. Not every rubber job needs them. I would not assume one setting fits every batch; even small changes in thickness or reinforcement can alter the cut.