
7 Best Titanium Waterjet Cutting Services for Global Buyers
Titanium looks simple on a specification sheet. On the shop floor, it can be less forgiving: a thin sheet may shift, a thick plate may demand a slower feed, and edge quality can vary with abrasive flow and nozzle condition. Titanium waterjet cutting offers a cold-cutting approach that avoids a heat-affected zone, but service quality still depends on setup, inspection, and operator skill.
Market context matters. Grand View Research’s Waterjet Cutting Machine Market report describes a growing global equipment market, while the U.S. Geological Survey’s Mineral Commodity Summaries 2025 tracks titanium supply and production. Neither report ranks service providers. That distinction matters: a machine-market forecast cannot prove that a particular shop will hold a tight tolerance. Abrasive-waterjet pioneer Dr. Mohamed Hashish’s research emphasizes the process’s cold-cutting character; for buyers, the practical question is how well each supplier controls taper, kerf, and surface finish on the specified grade and thickness.
This guide compares seven providers by capabilities, international support, documented quality practices, and quotation transparency. Ask for material traceability, sample-cut evidence, and realistic lead times. Small details count. A clean edge is useful; a clear inspection record is better. No shortlist replaces a test cut, and supplier claims deserve verification.
How Titanium Waterjet Cutting Works
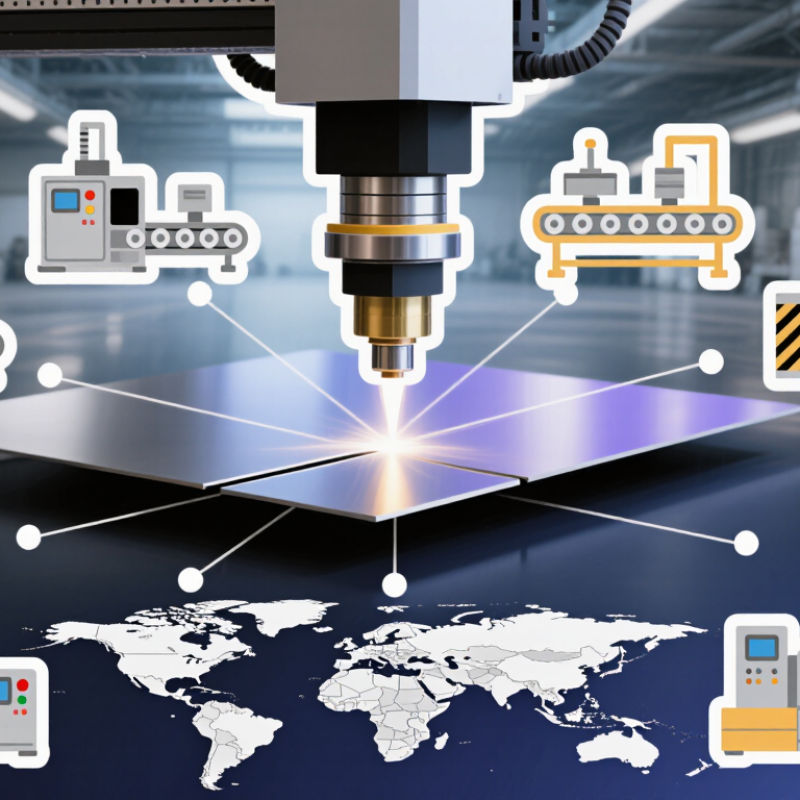
Titanium waterjet cutting begins with a digital drawing that guides a CNC-controlled cutting head. A pump pressurizes water, which exits through a tiny orifice at high speed. For titanium plate, abrasive particles are usually added to the stream to help cut through the metal. The process removes material without the intense heat of a torch or laser. The stream stays cool. That matters when a part must retain its original material properties near the cut edge.
Operators secure the sheet on a slatted table, check the nozzle, and set cutting speed for the alloy and thickness. Too much speed can leave rough striations; too little may widen the kerf or waste production time. Small details matter. A narrow bridge or sharp internal corner may need adjustment in the drawing to prevent movement during cutting. For critical parts, a trial cut can reveal edge taper and surface finish before the full sheet is processed. It is easy to assume every waterjet edge is ready to use. Often, inspection and light finishing are still needed, especially where parts must fit closely.
7 Best Titanium Waterjet Cutting Services for Global Buyers - How Titanium Waterjet Cutting Works
Titanium waterjet cutting typically uses a high-pressure water stream mixed with abrasive garnet to erode material along a programmed path. Because it is a non-thermal cutting process, it avoids the heat-affected zone associated with thermal cutting methods. Results depend on the alloy, thickness, machine setup, and drawing requirements.
| Service Type | How It Works | Typical Titanium Applications | Key Advantages | Points to Verify | Useful Buyer Questions |
|---|---|---|---|---|---|
| 1. Abrasive waterjet profile cutting | Abrasive particles carried by a focused water stream cut through titanium sheet or plate along a programmed 2D path. | Flat brackets, panels, gaskets, blanks, and custom contours in commercially pure titanium or titanium alloys. | No thermal heat-affected zone; suitable for complex profiles and a range of material thicknesses within the machine’s capacity. | Ask about achievable tolerances, edge taper, surface striations, and the supplier’s maximum thickness for the specified alloy. | Can you provide a cut sample or inspection report using material of the same grade and thickness? |
| 2. Precision small-part cutting | A fine, controlled abrasive stream follows closely spaced or intricate tool paths to produce small features and detailed outlines. | Instrument components, compact fixtures, prototypes, and parts with narrow slots or small internal contours. | Can create intricate 2D geometries without introducing heat from a conventional thermal cutting process. | Small holes and narrow features may be limited by material thickness, nozzle condition, and the relationship between feature size and kerf. | What minimum hole, slot, and feature sizes are practical for my material thickness? |
| 3. Multi-axis bevel cutting | A tilting cutting head changes angle during cutting to produce bevels or compensate for cut taper. | Parts requiring angled edges, prepared joints, or selected bevel features. | Can reduce or control taper and may create angled edges in the cutting operation. | Confirm the available cutting-head angle, achievable bevel accuracy, and whether the drawing requires a specific edge condition. | Can you machine the specified bevel in one setup, and how will you measure its angle? |
| 4. Prototype and short-run cutting | Parts are cut from customer drawings or CAD files, often with a focus on quick design iterations and low setup requirements. | Engineering samples, fit checks, replacement parts, and low-volume custom components. | Useful for testing geometry before committing to larger production quantities; changes can be made through the digital cutting program. | Clarify file formats, drawing revision control, inspection scope, and whether material certification is supplied. | Can you review the CAD file before cutting and confirm the revision used for production? |
| 5. Repeat batch production | Approved cutting programs and documented setups are reused to produce repeated lots of parts. | Recurring production of titanium sheet or plate components with stable specifications. | Supports repeat orders when the supplier controls program revisions, material identification, and inspection records. | Ask how the supplier monitors dimensional consistency, abrasive and nozzle condition, and lot traceability. | Can each shipment be linked to a material heat or lot certificate and an inspection record? |
| 6. Cutting with material traceability | Material identification and documentation are maintained through cutting and part handling. | Projects that specify a particular grade, such as commercially pure Grade 2 or Ti-6Al-4V Grade 5. | Helps buyers verify that supplied parts correspond to the specified material and documentation requirements. | Confirm the required certificate type, marking method, segregation practices, and whether traceability is maintained after nesting. | What material documents will be supplied, and how are cut parts kept associated with their source material? |
| 7. Cutting with secondary finishing | Waterjet-cut parts receive agreed follow-up work, such as deburring, edge treatment, cleaning, or dimensional inspection. | Components needing a specified edge condition, clean handling, or inspection before shipment. | Combines cutting with additional preparation steps, which can simplify coordination for the buyer. | Define the required finish clearly; waterjet-cut edges may show taper or striations, and finishing requirements vary by application. | Which finishing and inspection operations are included, and what acceptance criteria will be recorded? |
Related Posts
-
7 Tips for Titanium Waterjet Cutting Buyers?
-
What is Waterjet Cutting Titanium? Benefits, Process, and Applications Explained
-
Top 10 Benefits of Using Waterjet Garnet for Precision Cutting in 2023
-
Why Choose Waterjet Cutting Rubber for Your Manufacturing Needs?
-
Top Tips for Maintaining Waterjet Cutting Parts for Optimal Performance
-
Top Dock Hoist Solutions for Global Buyers in 2026?